To measure PCB V-score remaining thickness, use a suitable V-score web gauge to contact the opposing groove surfaces at a defined inspection location. Support the panel, verify the instrument, seat the contacts without forcing them, and record readings at the locations specified in your inspection plan.
Understand What V-Score Remaining Thickness Means
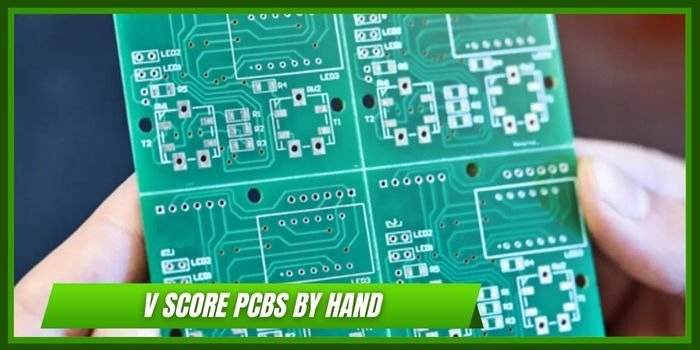
V-score remaining thickness is the material left between the upper and lower grooves of a double-sided scored PCB. It is also called residual thickness, web thickness, or V-cut remaining thickness.
This material keeps the boards connected as a panel until depaneling.
Remaining thickness is different from:
- Overall PCB thickness: The distance between the board’s outer surfaces.
- Upper groove depth: The depth of the score measured from the upper surface.
- Lower groove depth: The depth measured from the lower surface.
- Groove alignment: The relative position of the upper and lower scores.
For aligned grooves measured along the same local thickness direction, the geometric relationship is:
Remaining thickness = Local board thickness − Upper groove depth − Lower groove depth
Select a Measurement Method That Fits the Groove
For routine inspection, a dedicated V-CUT thickness tester or V-score web checker can provide direct measurements when its contacts fit the groove and reach the inspection location.
Other methods may be useful for investigation or verification.
| Method | Potential use | Main limitation to assess |
|---|---|---|
| Dedicated V-score web gauge | Routine remaining-thickness inspection | Contact geometry, alignment, force, and access |
| Separate board-thickness and groove-depth measurements | Indirect calculation where the geometry supports it | Matching locations, reference surfaces, and combined uncertainty |
| Prepared cross-section with optical measurement | Investigation of web geometry and groove alignment | Destructive preparation and section-location control |
| Standard caliper | General board dimensions | Standard jaws may not reach the required groove surfaces |
Step-by-Step Measurement Procedure
To ensure repeatable and reliable inspection data, follow this structured procedure:
Step 1: Instrument Calibration and Zeroing
- Power on the digital thickness tester and select the appropriate measurement unit (mm or mils).
- Clean the lower V-anvil and upper probe tip to remove dust, flux residue, or debris.
- Perform a zero-point check using a certified grade-0 gauge block or calibration standard matching your target board thickness range.
Step 2: Sample Selection and Preparation
- Collect sample panels from the designated sampling points of the production batch (typically start, middle, and end of a scoring machine run).
- Ensure the V-groove channels are clean and free of burrs, loose fiberglass strands, or heavy solder mask pooling that could skew the contact point.
Step 3: Positioning the Panel
- Place the test panel horizontally across the lower support stage.
- Carefully guide the V-groove channel over the specialized lower V-anvil so that it seats snugly and stably without rocking.
- Align the upper pointed or ball-tipped spindle directly above the corresponding top V-groove.
Step 4: Executing the Measurement
- Lower the upper spindle gently into the V-groove until it makes full contact with the thinnest point of the web.
- If using a motorized or counterweighted benchtop stand, allow the drop weight to apply consistent, repeatable downward force.
- Read and record the digital display value.
Step 5: Multi-Point Verification
- Measure at least three to five different locations along the V-score line (e.g., both outer edges and the center) to check for blade wear or uneven scoring depth across the panel.
5. Record Results and Apply the Correct Acceptance Rule
An inspection record should make it possible to identify what was measured and reproduce the method.
Include:
- Part number, drawing revision, lot, and panel identification.
- Score-line and measurement-point identification.
- Instrument identification and relevant contact configuration.
- Individual readings and units.
- Acceptance limits, disposition, operator, and date.
- Notes about contamination, damage, unstable seating, or repeat measurements.
Keep individual results even when you calculate an average or range.
6. Troubleshoot Unstable or Unexpected Readings
An unusual result can come from the panel, the measuring system, or the way the panel is loaded. Investigate before changing the scoring process.
| Observation | Possible explanation | Practical check |
|---|---|---|
| Reading changes after each reload | Inconsistent seating, support, or measurement position | Mark the location and repeat with controlled loading |
| Reading changes when the panel is tilted | Contact geometry or support affects the measurement | Check seating and remove unintended bending |
| Unexpectedly high reading | Contact on a groove flank, contamination, or a genuinely thick web | Inspect the contact area and confirm with a suitable method |
| Unexpectedly low reading | Damaged web, contact indentation, setup error, or a genuinely thin web | Check the reference, contact condition, and panel |
| Readings vary along the score | Actual process variation or changing measurement conditions | Repeat mapped locations with the same setup |
| Zero changes during inspection | Contamination, movement, temperature change, or instrument condition | Stop, verify the instrument, and assess affected results |
 French
 English
 German
 Spanish
 Vietnamese
 Russian